Explore our factory-direct, highly customisable aluminium cabinet solutions engineered for hotel, residential, outdoor, and specialized commercial applications.
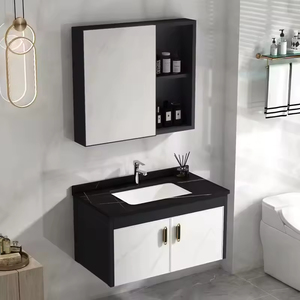
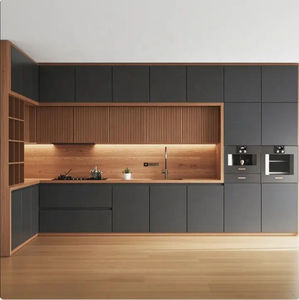
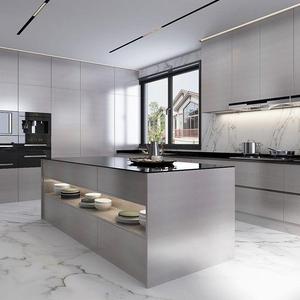
In the modern architecture, hotel fit-out, and commercial real estate sectors, material selection directly influences lifetime maintenance costs, asset longevity, and indoor environmental performance. Traditional wooden cabinet substrates—such as Medium-Density Fibreboard (MDF), particleboard, and plywood—are structurally limited when exposed to ambient humidity, thermal fluctuation, insect infestation, and strict fire safety regulations. Consequently, structural aluminium cabinetry has transitioned from a niche industrial solution to a dominant global procurement standard.
As leading fabricators operating facilities in Al Sajaa Industrial Area, Sharjah, and supplying projects throughout Dubai, Abu Dhabi, and international markets, Skyline Aluminium delivers high-precision extruded aluminium cabinet systems tailored to the rigorous demands of tropical, coastal, and high-traffic environments. This whitepaper analyzes the metallurgical advantages, manufacturing standards, future procurement trajectories, and the global manufacturer evaluation matrix necessary for project specifiers, developers, and wholesale buyers.
When specifying cabinetry for residential towers, luxury villas, commercial pantries, or specialized outdoor equestrian installations, structural engineers and interior architects balance initial procurement costs against lifetime asset performance. The comparative analysis below outlines the technical metrics driving the industry shift toward 6063-T5 aluminium alloy systems.
| Performance Metric | Aluminium Alloy (6063-T5) | Moisture-Proof MDF / Plywood | Stainless Steel (304 Grade) |
|---|---|---|---|
| Moisture & Water Resistance | 100% Waterproof (Zero Swelling) | Delaminates / Swells under prolonged moisture | 100% Waterproof (Risk of pitting in high salinity) |
| Termite & Biological Decay | Immune to insect & fungal attack | Highly vulnerable without chemical treatment | Immune |
| VOC & Formaldehyde Off-Gassing | Zero Formaldehyde Emission (E0 Standard) | Emits formaldehyde binder resin gases | Zero Formaldehyde Emission |
| Fire Safety Rating | Class A1 Non-Combustible | Combustible (Requires fire retardant coating) | Class A1 Non-Combustible |
| Structural Weight-to-Strength Ratio | Superior (Lightweight & High Tensile) | Heavy (High floor load requirement) | Heavy (Difficult mobilization) |
| Finish Customization & Texture | Anodized, Powder Coat, Wood Sublimation | Veneer, Laminate, Paint | Brushed, Polished, PVD Coating |
| Recyclability & Circular Economy | 100% Infinitely Recyclable | Non-recyclable (Landfill waste) | 100% Recyclable |
Driven by ESG (Environmental, Social, and Governance) mandates, architectural automation, and prefabrication methodologies, the commercial cabinet industry is experiencing four transformative developments:
Developers are moving away from traditional on-site carpentry in favor of Ready-to-Assemble (RTA) and pre-engineered aluminium joinery. CNC precision cutting and modular profile interlocks allow rapid assembly, reducing on-site installation labor by up to 60% while ensuring sub-millimeter tolerances across hotel suites and high-rise developments.
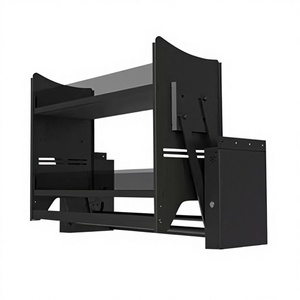
Modern luxury interior specifications demand seamless integration of smart home hardware. Motorized drop-down baskets (such as electric lifting seasoning racks), touchless sensor-activated cabinet doors, and integrated LED thermal management channels are becoming standard baseline requirements for premium kitchen and wardrobe systems.
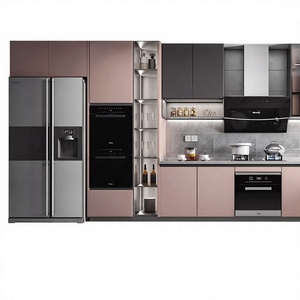
The aesthetic barrier of cold industrial metal has been overcome through Qualicoat-certified powder coatings and 3D wood-grain thermal transfer technology. Furthermore, modern designs blend structural aluminium frames with ultra-thin sintered stone tops, fluted tempered glass doors, and soft-touch anti-fingerprint anodized facings.
Operating from our dedicated fabrication facility in Industrial Area – Shed No. 3 & 4, Al Sajaa, Sharjah, Skyline Aluminium bridges the gap between precision manufacturing and site implementation. With over 12 years of hands-on experience across the seven emirates of the UAE, our engineering workflow ensures that every aluminium cabinet system performs impeccably under regional heat, extreme humidity, and high usage frequency.
We maintain end-to-end control over extrusion cutting, double-mitre jointing, CNC routing, hardware machining, and final assembly. Operating without third-party subletting guarantees strict adherence to project specifications and zero lead-time drift.
Our surface finishing options include sea-sky resistant anodizing, marine-grade Qualicoat Class 2 powder coatings, and realistic timber-look sublimation—ensuring long-term color fastness without peeling, cracking, or UV chalking.
From initial shop drawing approval and mill test certificate verification to final factory mock-up sign-off, every cabinet batch undergoes stringent inspection for structural integrity, door alignment, and silent soft-close drawer action.
When selecting an OEM, ODM, or direct architectural supplier for large-scale developments, procurement teams must look beyond initial unit pricing. Ensure your prospective vendor meets the following critical operational criteria:
Technical guidance and sourcing clarity provided by our senior engineering and manufacturing team.
Answer: Modern architectural aluminium cabinets are engineered specifically to eliminate metallic noise. By combining high-density aluminium honeycomb core insulation inside cabinet door panels, soft-close hydraulic European hinges, and perimeter silicone seal gaskets, door closure is completely silent and provides a solid, premium tactile feel similar to solid wood.
Answer: Aluminium is inherently superior to wood and steel in coastal or tropical climates. When treated with marine-grade Qualicoat powder coating or anodized finishes, aluminium frames develop a passive protective oxide layer that renders them 100% rust-proof, salt-air resistant, and immune to ambient humidity swelling.
Answer: Yes. Advanced 3D vacuum thermal transfer technology allows us to apply realistic, textured wood-grain finishes that replicate oak, walnut, and teak aesthetics while retaining metal durability. Furthermore, frames easily integrate fluted glass, frosted safety glass, sintered stone, or leather-textured aluminium composite panels.
Answer: Standard custom cabinet packages for villas or low-rise commercial fit-outs are fabricated within 2 to 3 weeks following shop drawing and dimensional site survey approval. Large-scale bulk contract orders are delivered in scheduled phases aligned with the main project construction schedule.
Answer: Absolutely. Aluminium cabinetry produces zero volatile organic compounds (VOCs) and zero formaldehyde emissions (achieving strict E0 indoor air quality standards). Unlike timber boards bonded with urea-formaldehyde resins, aluminium is non-toxic, chemically inert, and 100% infinitely recyclable at the end of its product lifecycle.
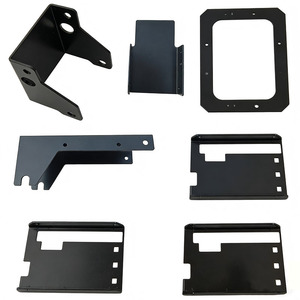
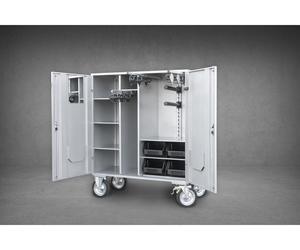
Answer: Yes. Beyond residential kitchen cabinetry, our factory manufactures custom sheet metal equipment enclosures, dustproof/waterproof outdoor electrical cabinets, equestrian horse tack trunks, and specialized hospital/laboratory storage units fabricated to ISO 9001 specifications.
Submit your architectural elevation drawings, bill of quantities (BOQ), or custom dimensional requirements today. Our engineering team in Al Sajaa, Sharjah provides complimentary technical reviews, shop drawing estimation, and competitive factory-direct quotations.